Author: chshim39@hotmail.com

  • After You Submit the Quotation: The Documents Buyers Expect from a Korean Supplier

    After You Submit the Quotation: The Documents Buyers Expect from a Korean Supplier

    Sending the quotation is not the end of the RFQ process. Once the price is in, the buyer wants to see how the supplier will actually do the work. In practice, this means a set of documents that the supplier prepares by reading the RFQ package and the drawings carefully. The buyer reviews them before deciding whether to place an order.

    If you are an overseas buyer evaluating Korean suppliers, these documents are your preview of how the project will run. If a supplier cannot produce them clearly, that tells you something. This is the second part of a short series. The first part, What an RFQ Really Is, and What a Korean Supplier’s Response Tells You, explains what the RFQ contains and how a supplier should respond to it.

    Schedule and responsibility

    Company profile. The basic starting point: who the company is, what it makes, and who its customers are.

    Timing schedule. A schedule showing the major steps from design through shipment. It is one of the most important documents in a project, and the one I would look at first. See how project timing and schedule work in practice.

    Contact points. Who is responsible for what during the project? A named person for each area, such as engineering, quality, production, and shipping, means problems have an owner. Without it, questions go in circles.

    Manufacturing and subcontractors

    Manufacturing process flow. How will the quoted item actually be made, step by step? This shows whether the supplier has thought through the work before accepting it.

    In-house or outsourced. The RFQ documents and drawings usually highlight certain processes, such as painting and heat treatment. The buyer wants to know whether the supplier performs each of these itself or uses a subcontractor. The same question applies to materials and components, such as bolts and nuts: who supplies them?

    Supplier control plan. If subcontractors are involved, how will the supplier manage and control them? A supplier that outsources painting or heat treatment is still responsible for the result.

    Quality, people, and design

    Operation work sheets and skilled workers. Who will do the work, and how? An operation work sheet describes the steps, and the supplier shows which skilled workers are assigned to them. It shows that the work does not depend on guesswork.

    Quality assurance plan. How will quality be controlled from incoming material to final inspection, and how will the supplier prove it?

    Design resources. If the buyer entrusts the design to the supplier, who are the design engineers? Where design rules apply, this shows the supplier can follow them. If the supplier outsources part of the design, how will it manage that work?

    What buyers should know: documents only matter if they reach the shop floor

    Preparing and submitting these documents is not easy, especially for suppliers outside the large companies. Reviewing the RFQ package, writing each document, and keeping it accurate takes real effort. This is one reason many Korean manufacturers find it hard to deal with overseas buyers.

    But the documents themselves are not the point. What matters is that what is written is actually carried out in production. A process flow that nobody follows, or a quality plan the shop floor has never seen, has no value. When you review a supplier’s documents, ask how each one is reflected in the daily work.

    Not every buyer requires every document. It depends on the project and the buyer, case by case. Even so, a supplier that wants to work with overseas buyers is better off having these documents ready before the first RFQ arrives, rather than building them under deadline pressure.

    When the standards differ

    In the United States, buyers commonly rely on ASTM standards for technical requirements such as materials, coating, and heat treatment. Korean suppliers often work with Korean Industrial Standards (KS), which are separate standards with their own content.

    When the two do not match, the supplier cannot simply assume they are equivalent. The supplier should compare the Korean standard with the ASTM requirement, or with the relevant international standard, and explain to the buyer why the difference causes no problem. Work should begin only after the buyer confirms in writing that the comparison is acceptable. Raise this at the quotation stage. A short discussion early is far cheaper than a dispute after production.

    From documents to purchase order, and from purchase order to production

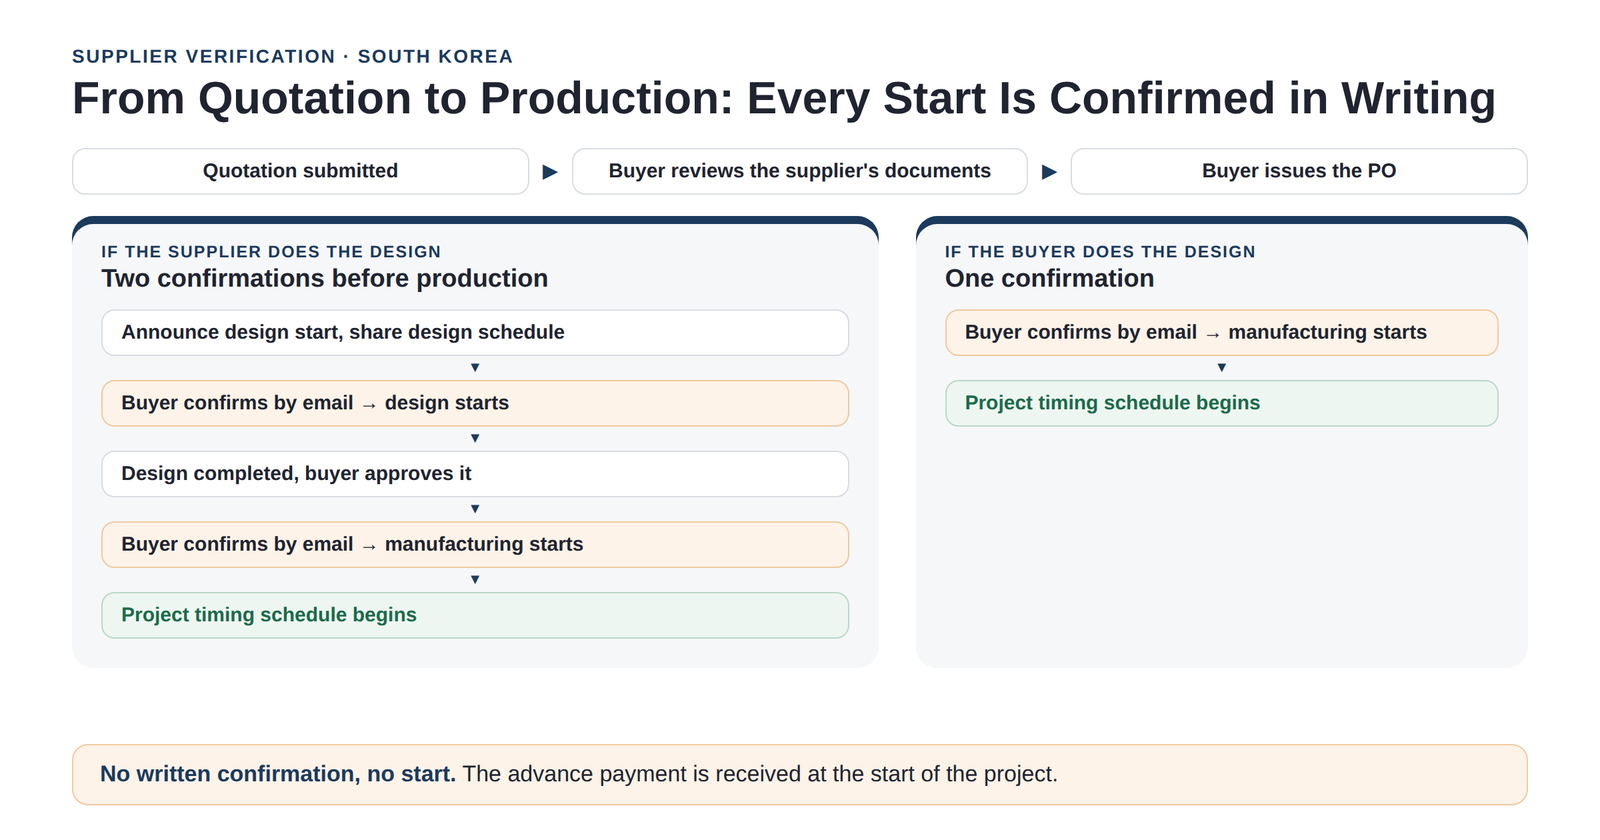
    When the buyer has reviewed these documents and is satisfied, the buyer issues a purchase order (PO). The PO is the formal start of the commitment, but the work does not begin until each step is confirmed in writing.

    If the buyer has entrusted the design to the supplier, the supplier first tells the buyer that the design stage is about to begin, shares the schedule, and prepares a timing schedule for the design work. The supplier then emails the buyer to say it is ready to start and asks the buyer to confirm. Design begins only after the buyer’s confirmation email arrives.

    When the design is finished, the buyer’s design engineer or other responsible person reviews it. Once the design is approved, the supplier again waits for a confirmation email before manufacturing starts. From that point, the project timing schedule takes over as the working tool for the rest of the project.

    If the buyer handles the design, the sequence is shorter. After the PO, the supplier waits for the buyer’s confirmation email before manufacturing begins.

    This rule is not a formality. In many projects, the advance payment is received at the start, so the supplier should never begin work without the buyer’s written confirmation. The same email protects both sides: the buyer knows exactly when the project has started, and the supplier knows the buyer is ready.

    What this means for buyers

    A supplier’s quotation shows its price. These documents show its way of working. Before you place a PO with a Korean manufacturer, make sure you have seen them, and make sure they match what the RFQ asked for. If a supplier says only that its own standard is fine, treat that as a warning sign. A reliable supplier shows the comparison and waits for your confirmation.

    If you would like help reviewing a supplier’s document package, see our Services or get in touch.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • What an RFQ Really Is, and What a Korean Supplier’s Response Tells You

    What an RFQ Really Is, and What a Korean Supplier’s Response Tells You

    Many buyers think of an RFQ as a simple price request. It is not. A Request for Quotation is a package of documents that defines exactly what the buyer needs, and the way a supplier handles that package tells you a lot about how they will handle your project.

    What is actually inside an RFQ

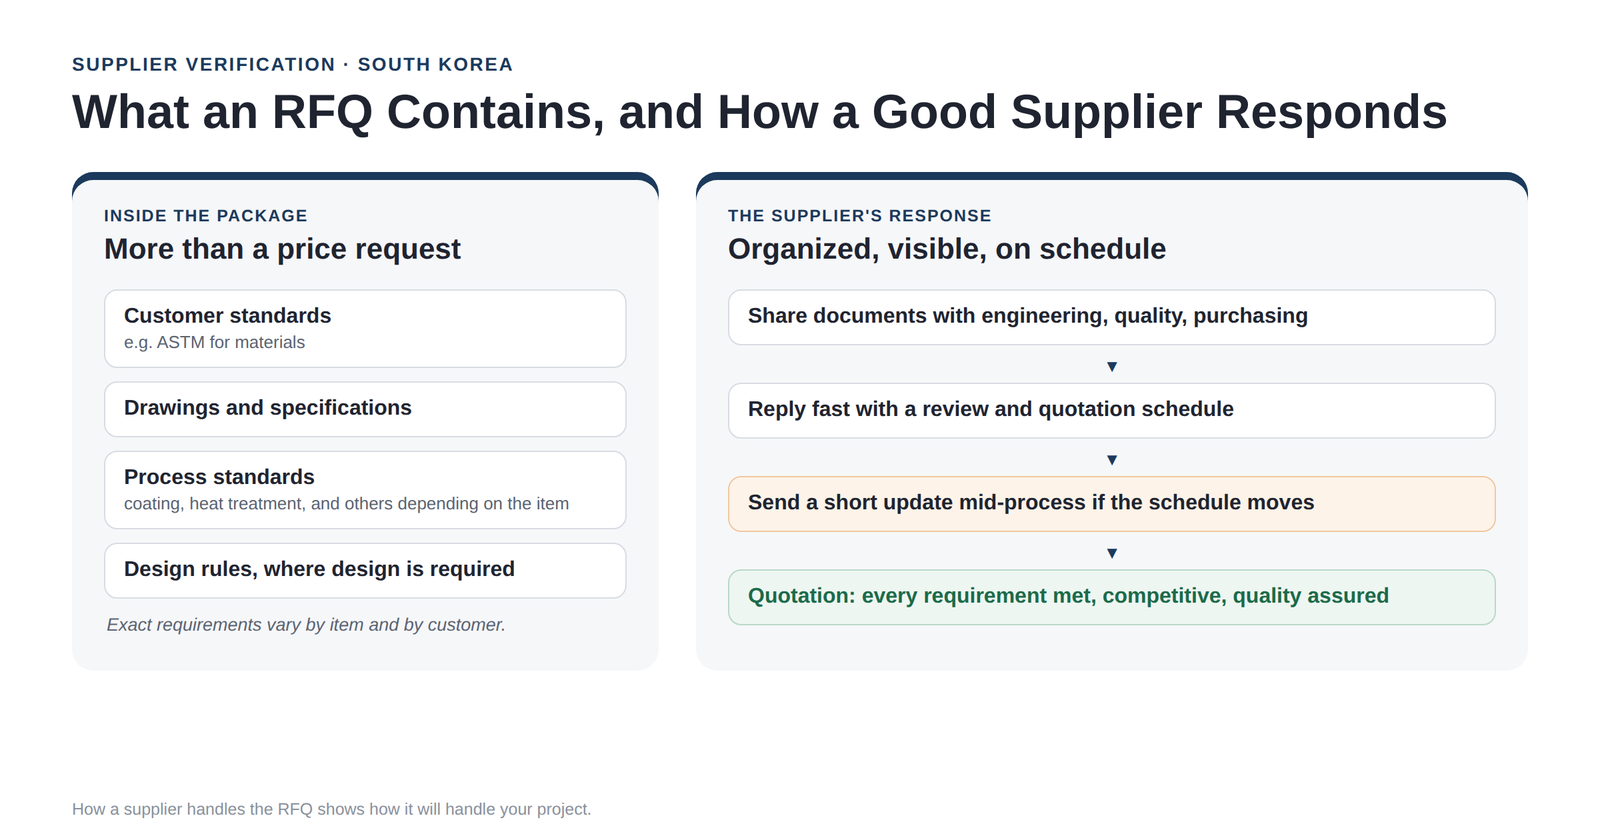
    A real RFQ contains every standard and specification that applies to the item being quoted. If the item is a steel structure or a piece of machinery and the customer is in the United States, the package typically includes American standards, such as ASTM specifications for the steel. If the preliminary drawing calls for painting on some surfaces and heat treatment on others, the coating specification and the heat treatment standard are in the package too, along with any other standards that apply to the item. Where design work is required, the design rules must be followed as well. The same applies whether the product is an automotive part or industrial equipment.

    So the supplier is not just pricing a product. They are being asked to confirm that every customer requirement can be met, and to reflect all of it in the price.

    Receiving an RFQ already says something

    A buyer who sends an RFQ generally already has real information about the company. Often that comes from a process audit or a factory visit that qualified the supplier to bid. Being invited to quote means the supplier has passed a first level of checking. As a supplier, it means the buyer is serious. As a buyer, it means your own screening comes first, and the RFQ is the next step in the evaluation.

    Why quoting is harder than it looks

    A good quotation has to do three things at the same time. It must reflect every requirement in the documents. It must be competitive against other suppliers. And it must come with a quality commitment the supplier can actually keep. That is a lot to review, and a supplier that does it carefully will often look slower than one that simply sends a number.

    How a well-organized supplier handles an RFQ

    Companies with a proper team do not leave the RFQ on one person’s desk. They distribute the documents to the relevant people, such as engineering, quality, and purchasing, so each part is reviewed by someone who understands it.

    They also do not make the buyer wait in silence. They reply quickly with a schedule: when the review will be finished and when the quotation will be submitted. Only then do they begin the internal review.

    If the review takes longer than planned, they say so before the deadline. A short update by email in the middle of the process is one of the simplest and most effective habits. When a buyer knows the schedule may move and why, they usually understand. When a buyer hears nothing, they assume the worst.

    If the buyer has a required date, the two sides agree on a schedule together. A supplier that negotiates a realistic date is usually more reliable than one that agrees to anything.

    What a Korean supplier’s RFQ response tells you

    Before you visit any factory, the way a supplier responds to your RFQ can show you:

    • Whether they acknowledge the request quickly and give you a clear schedule
    • Whether they read the whole document package, including the specifications, not only the drawing
    • Whether they ask clarifying questions instead of guessing
    • Whether they keep you informed during the review
    • Whether the quotation reflects your standards or only gives a price

    A supplier that does these things is organized, understands international requirements, and treats communication as part of the work. A supplier that sends only a low price with no questions may not have read the specifications, and that is a risk you want to see before an order, not after.

    Where this fits in supplier verification

    The RFQ response is one piece of a larger picture. It works best alongside the checks described in How We Select a Korean Manufacturer and Two Red Flags Most Buyers Miss, and you can score what you see with the free Supplier Verification Checklist.

    If you are preparing an RFQ for Korean suppliers and want help reviewing the responses, get in touch.

    Next in this series: After You Submit the Quotation: The Documents Buyers Expect from a Korean Supplier


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • Supplier Verification Checklist: Two Red Flags Most Buyers Miss

    Supplier Verification Checklist: Two Red Flags Most Buyers Miss

    A supplier checklist is a good place to start. It tells you what to look at. But a supplier can pass a checklist and still cause trouble once the project begins. In my experience, the risk tends to hide in two places that a checklist rarely captures: what happens after an audit finds a problem, and how the supplier communicates with you.

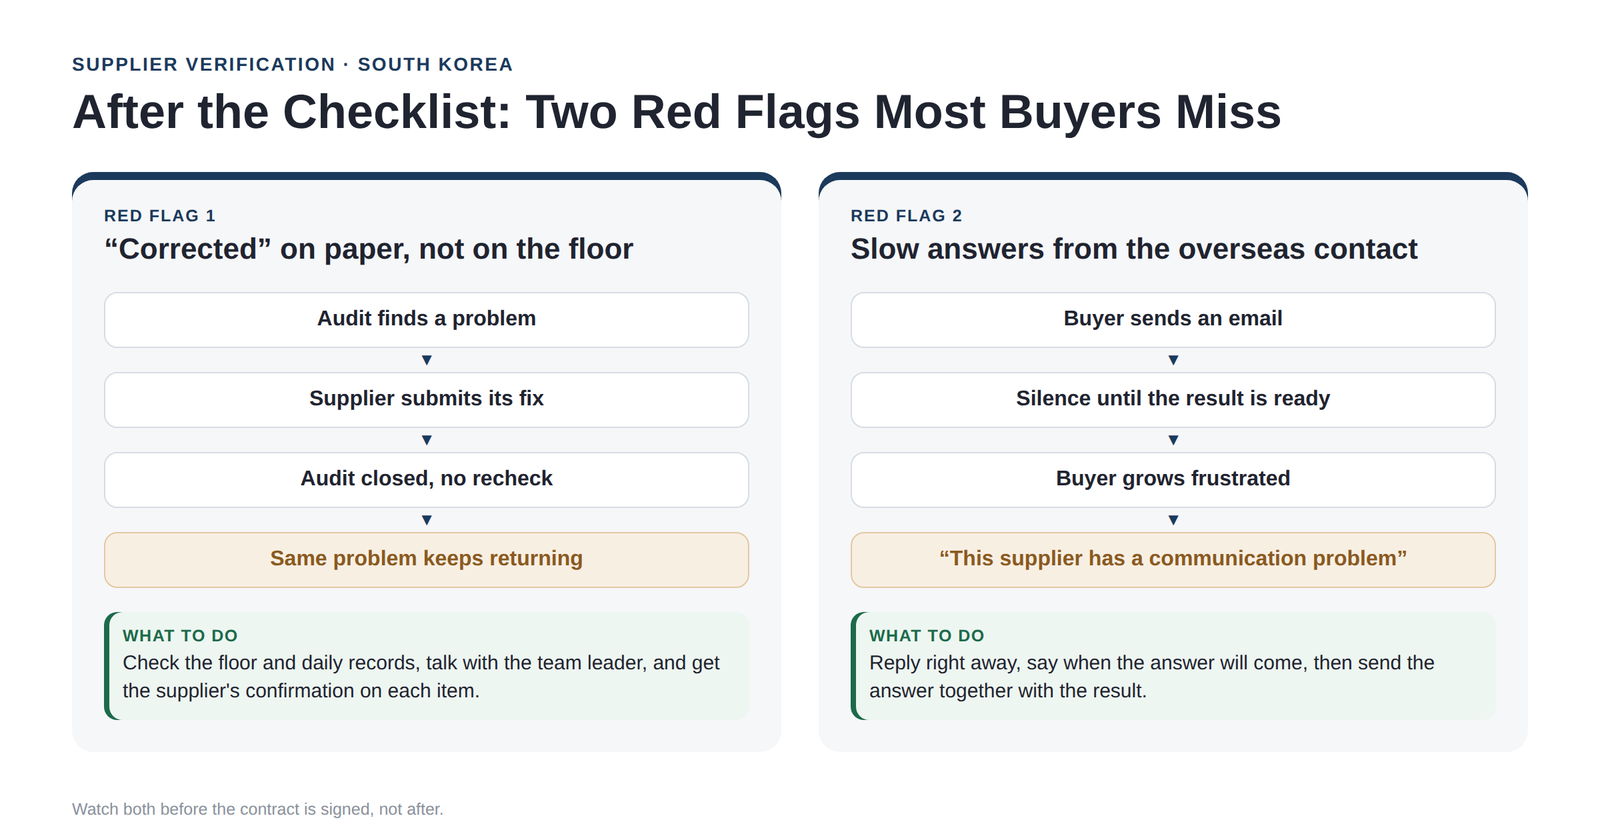
    Red flag 1: “Corrected” on paper, but the problems keep coming back

    Here is how many audits end. The auditor goes through the supplier with a checklist, records the problem areas, and reports them to the company. The company fixes or improves those items and submits its response to the auditor. In many cases, that is where it stops.

    Ideally, the auditor would visit once more to confirm that the improvements actually reached the shop floor. Some do. But often the auditor takes the company at its word, decides the problem has been resolved, and closes the audit.

    The difficulty is that even a real improvement is hard to judge from a document. The auditor may not know the process well enough technically to tell whether the fix addresses the true cause. And no one outside the company can be sure whether the change was made from the right point of view: one that solves the problem for the buyer, or one that merely closes the finding. Buyers then end up asking the same question: we were told this was improved, so why does the same problem keep happening?

    This is where problems most often arise, so it deserves close attention:

    • Do not treat a submitted corrective response as proof. Read what exactly was changed and why.
    • Check whether the change shows up on the floor and in the daily records, not only in a revised document.
    • Spend real time talking with the supplier’s responsible team leader. Those conversations often reveal whether the team understands the cause of the problem.
    • Get the supplier’s confirmation on each corrected item before you rely on it.

    Realistically, an audit cannot run for days on end. That is exactly why the time you do have should go to the items that failed, and to confirming that the fix is real.

    Red flag 2: Slow answers from the overseas contact

    These days, even small and mid-sized Korean manufacturers rarely have a serious English problem. The more common risk is a person in the overseas contact role who has little experience with overseas buyers. If they do not understand how overseas buyers think and work, the project can become difficult in unexpected ways.

    The best remedy is fast feedback. When I handled overseas sales, I would read a buyer’s email in the morning and reply right away: we have received it, and after meeting with the team we will get back to you by a specific date. Then I held the meeting and sent the answer together with the result. The buyer sees that someone is paying attention to their email, and when the result arrives, concludes that this contact can be trusted.

    The common pattern is the opposite. The contact waits until the result is ready and only then replies. In the meantime, the buyer hears nothing and grows frustrated. After a few rounds of this, the buyer decides that the supplier has a communication problem.

    Real communication is simple: read the email, make a judgment, reply quickly, then gather the answer with the relevant team and send it. When you evaluate a supplier, watch how fast and how clearly the overseas contact responds before the contract is signed, not after.

    Where the checklist fits

    A checklist is still worth using. It organizes what to look at across documents, on-site checks, finances, and communication. My free Supplier Verification Checklist covers twelve items across those areas and gives you a quick read on how well screened a supplier is.

    The two red flags above are what I look for beyond the checklist when I audit and manage suppliers. To see how an on-site audit works, read What a Manufacturing Process Audit in South Korea Actually Looks Like. To see how I combine sourcing, audit, and project management, visit the Services page.

    For a real project where schedule and quality were tested under pressure, read the case study Building a Truck Wash System for a Kazakhstan Copper Mine, or see why the same client came back for a second project.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • What a Manufacturing Process Audit in South Korea Actually Looks Like

    What a Manufacturing Process Audit in South Korea Actually Looks Like

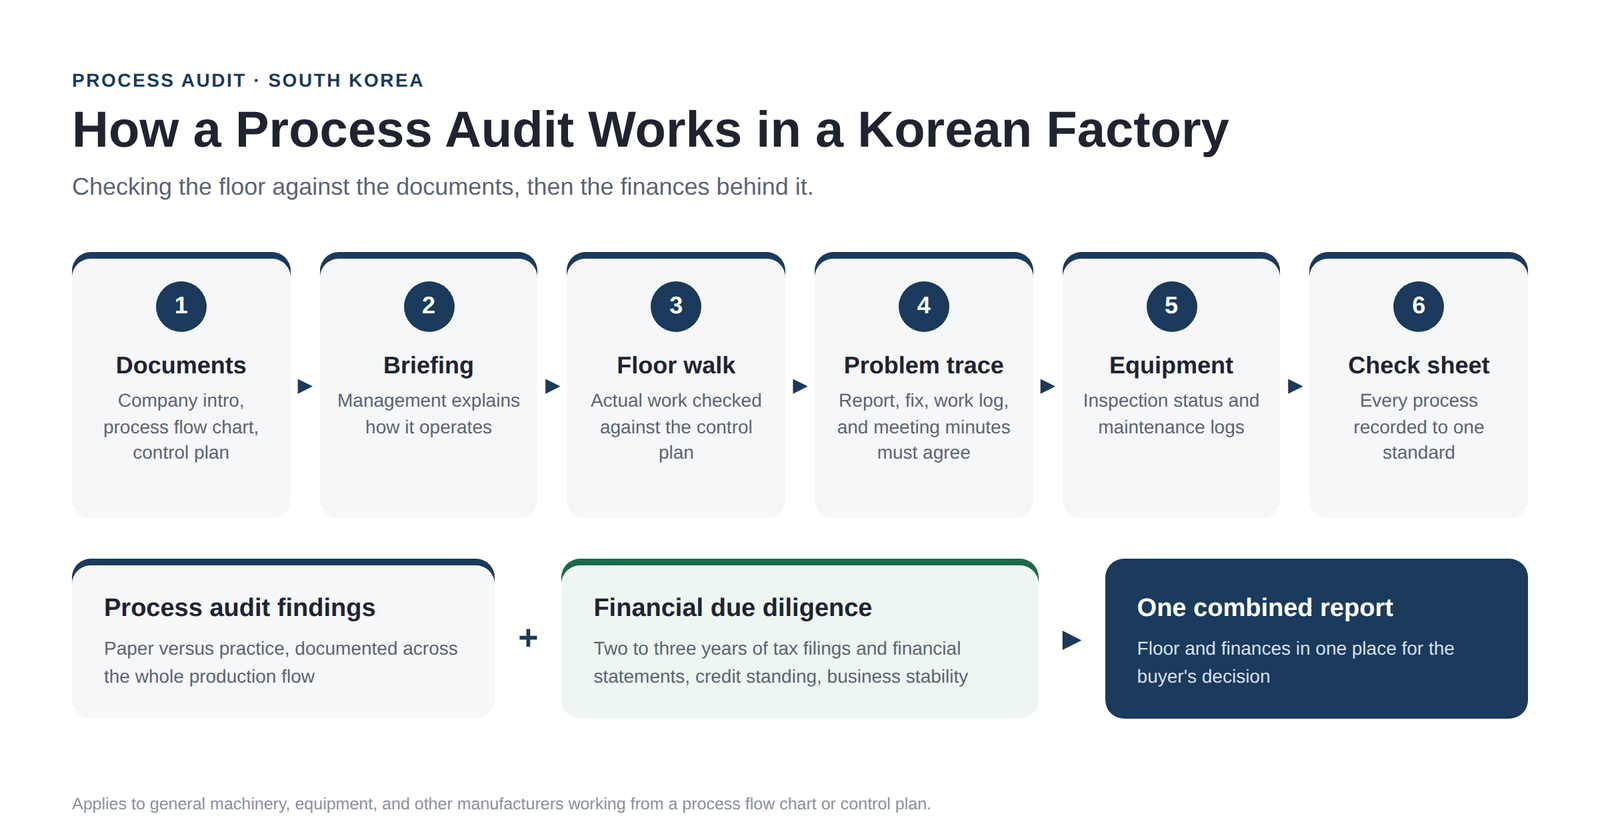
    Many overseas buyers hear “we’ll audit the factory” and picture a clipboard and a quick tour. In practice, a proper process audit in Korea is a structured comparison between what the factory says it does and what actually happens on the shop floor. Here is how it works, based on the audits I have run on Korean suppliers.

    Step 1: Documents come first

    Before anyone visits the site, I request the supplier’s core documents: the company introduction, the manufacturing process flow chart, and the control plan. The control plan is the key one. It defines, process by process, what is checked, how often, and what happens when something goes wrong. Everything on the floor is measured against it.

    Step 2: The visit begins with the company, not the factory

    On audit day, the supplier first presents the company: what they make, who they supply, and how they are organized. This is not small talk. It tells me how the management understands its own operation, and it sets up the questions I will ask during the walk-through.

    Step 3: Walking the floor with the control plan in hand

    Then we walk the actual production line, with the process flow chart and the control plan in hand. I carry my own check sheet too, but in practice the two are very similar, because the check sheet is built on the control plan’s standards. The core question at every station is simple: is the work being done the way the documents say it is?

    Step 4: Following a problem all the way through

    This is where an audit gets real. I do not stop at “is there a procedure.” I follow what happens when something goes wrong:

    • Was the problem reported to the people above the operator?
    • After the report, was the process actually corrected?
    • Does the correction show up in the daily work log?
    • Do the work log and the meeting minutes from the problem meeting tell the same story?
    • On the floor today, has the problem really been fixed?

    A supplier can have a perfect procedure on paper. If the work log says one thing and the meeting minutes say another, or if the fix never reached the line, that gap is exactly what the audit exists to find.

    Step 5: Equipment and maintenance records

    At each process I also check the machine in use: has it been inspected, and is there a maintenance log to prove it? Each item goes on the check sheet, one by one. A machine that runs well today but has no inspection record is a risk, because the next breakdown will have no history to learn from.

    Step 6: Recording everything on the check sheet

    By the end of the walk, every process has been checked against the same standard and recorded. The result is not an impression, it is a documented comparison of paper versus practice for the whole production flow.

    A process audit alone is not enough: financial due diligence and the report

    Even a well-run floor can sit inside a financially fragile company, and that risk can surface in the middle of your project. So I pair the process audit with financial due diligence. I analyze the supplier’s tax filings and financial statements for the last two to three years, along with credit standing and business stability, to confirm you are getting not just a capable factory but a stable one.

    The on-site audit findings and the financial due diligence results are combined into a single report for the buyer. You see the paper-versus-practice comparison, what was observed on the floor, and the supplier’s financial position in one place, and can make your decision from there.

    Which suppliers does this apply to?

    This approach applies to general machinery and equipment manufacturers, and to any manufacturer that works from a process flow chart or control plan. The industry changes, but the logic of the audit does not: check the floor against the documents.

    What this means for buyers

    If a supplier can show you consistent documents, a floor that matches them, a clear trail from problem to correction, and a stable financial position, you are looking at a supplier that manages itself. If not, you want to know before the purchase order, not after.

    For how this fits into a full supplier evaluation, read Sourcing Korean Suppliers: Two Paths for Overseas Buyers. To see how I combine sourcing, audit, and project management, visit the Services page.

    For a real project where these checks mattered, read the case study Building a Truck Wash System for a Kazakhstan Copper Mine, where wrong site drawings were caught before fabrication and the system passed the client’s audit on schedule.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • Sourcing Korean Suppliers: Two Paths for Overseas Buyers

    Sourcing Korean Suppliers: Two Paths for Overseas Buyers

    When an overseas buyer starts looking for a Korean manufacturing partner, the first challenge is usually "who do I go through to find suppliers?" A quick Google or AI search typically surfaces trade-related organizations or large consulting firms that provide supplier lists. What’s harder to see from the outside is how that list is actually built, and what gets verified once you have it.

    This matters most for buyers sourcing specific categories — machinery, piping, structural components, and similar — because choosing the wrong supplier can turn into real project risk: delayed delivery, quality issues, or in the worst case, lost deposits.

    This post compares two paths — the way large consulting firms are commonly known to operate, and the integrated service KorealiaisonPM provides.

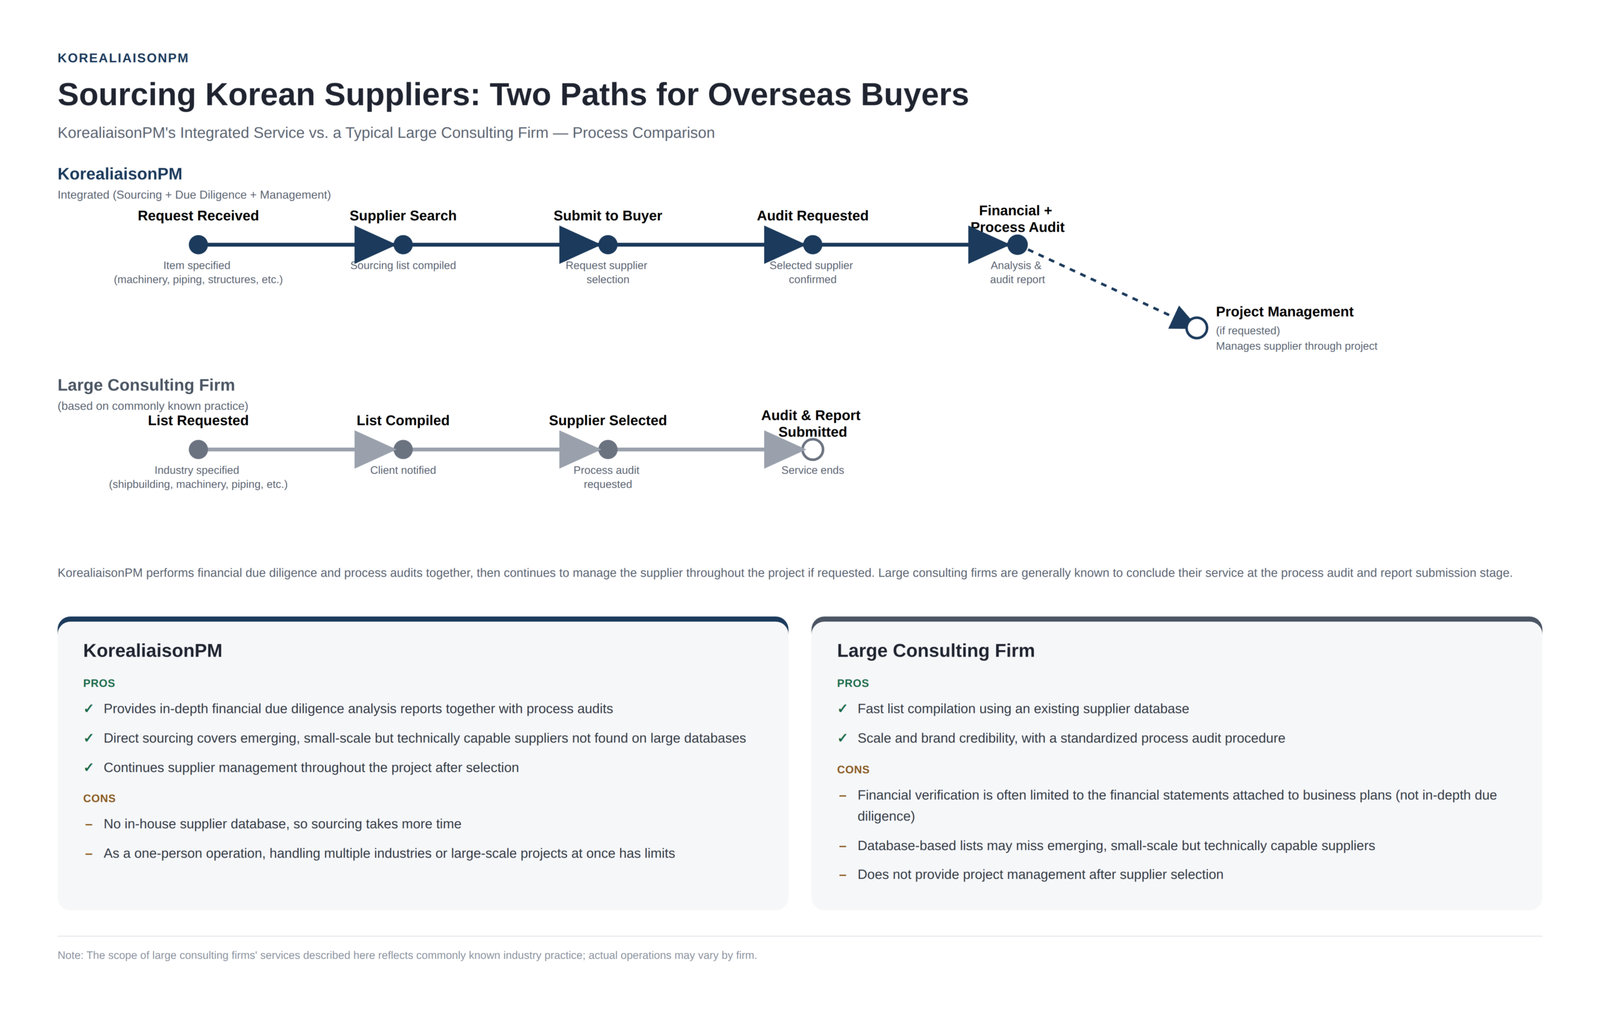
    Comparison diagram of two paths overseas buyers use to source Korean suppliers: a large consulting firm's process versus KorealiaisonPM's integrated sourcing, due diligence, and project management service

    Path 1: Going Through a Large Consulting Firm

    The process generally works like this:

    1. The overseas buyer specifies a category (machinery, piping, structures, etc.) and requests a supplier list.
    2. The consulting firm compiles a list from its existing supplier database and delivers it to the client.
    3. Once the buyer selects a supplier from the list, the firm carries out a process audit.
    4. The audit report is submitted, and the service is generally understood to end there.

    Pros

    • Fast list compilation, since the firm already has a supplier database. Useful when timelines are tight.
    • Scale and brand credibility, backed by a standardized process audit procedure.

    Cons (based on commonly known practice)

    • Financial verification is often limited to the financial statements attached to the supplier’s business plan — a different level of scrutiny than in-depth due diligence.
    • Because the list is database-based, emerging or small-scale suppliers with strong technical capability may never make it onto the list in the first place.
    • The firm’s role typically ends at supplier selection and process audit; project management after that point is usually not included.

    Path 2: KorealiaisonPM’s Approach

    KorealiaisonPM combines the front end of this process (supplier discovery and listing) and the back end (financial due diligence and process audit) into a single continuous workflow, and adds ongoing project management on top of it.

    1. The buyer’s requirements are received (e.g. machinery, piping, structures).
    2. Suppliers are sourced directly and a shortlist is compiled. This takes more time than pulling from an existing database, but allows for a broader and more careful search.
    3. The shortlist is submitted to the buyer.
    4. Once the buyer selects candidates, an audit is requested and carried out.
    5. Financial due diligence is performed and documented in an analysis report, alongside a process audit and its report.
    6. The service doesn’t end there — if the buyer requests it, supplier management continues for the duration of the project.

    Pros

    • In-depth financial due diligence analysis, delivered together with the process audit — a step beyond checking business-plan-level financial statements.
    • Because sourcing is done directly rather than pulled from a database, emerging and small-scale suppliers with real technical capability can be included.
    • Supplier management continues throughout the project after selection, so progress isn’t lost once the contract is signed.

    Cons

    • No in-house supplier database, so sourcing takes more time.
    • As a one-person operation, handling multiple industries or very large-scale projects simultaneously has its limits.

    What Buyers Should Check Before Committing

    Whichever path fits your project, it’s worth confirming a few things before signing on:

    • Is the supplier list built from an existing database, or sourced directly?
    • Is financial verification limited to business-plan-level statements, or does it include a deeper analysis report?
    • Does the service include supplier management once the project is underway, or does it end at the audit report?

    Closing Thoughts

    Note: The description of large consulting firms above reflects commonly known industry practice; actual operations may vary by firm.

    Both paths have their place. If you need fast, standardized list compilation, a large consulting firm may be the better fit. If you want a broader search that includes suppliers outside the usual databases, combined with deep financial due diligence and continuous project management, KorealiaisonPM’s approach may serve you better.

    If you’re planning to source from Korea, it’s worth starting by figuring out which path actually fits your project.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • How KoreaLiaisonPM Actually Selects a Korean Manufacturer

    How KoreaLiaisonPM Actually Selects a Korean Manufacturer

    A few years ago, a buyer had already signed with a Korean supplier through a different sourcing agency. The certifications were there. The quote was reasonable. On paper, everything checked out. But a few months into production, problems from aging equipment started showing up again and again. Nothing in the paperwork had flagged it. A certificate tells you what a piece of equipment is capable of — not what it’s actually doing right now.

    “How do you choose the right factory?” It’s the question I get more than any other from overseas buyers. Most people underestimate how hard this question really is. Finding a list of Korean manufacturers takes a few searches. The hard part is knowing which one is worth staking your project, your budget, your timeline — and ultimately your reputation — on.

    Over the past year, I’ve written about different pieces of this process separately — the red flags I watch for, why financial due diligence matters as much as a factory audit, what actually happens once production starts. This post pulls those pieces together into the sequence I actually follow, start to finish.

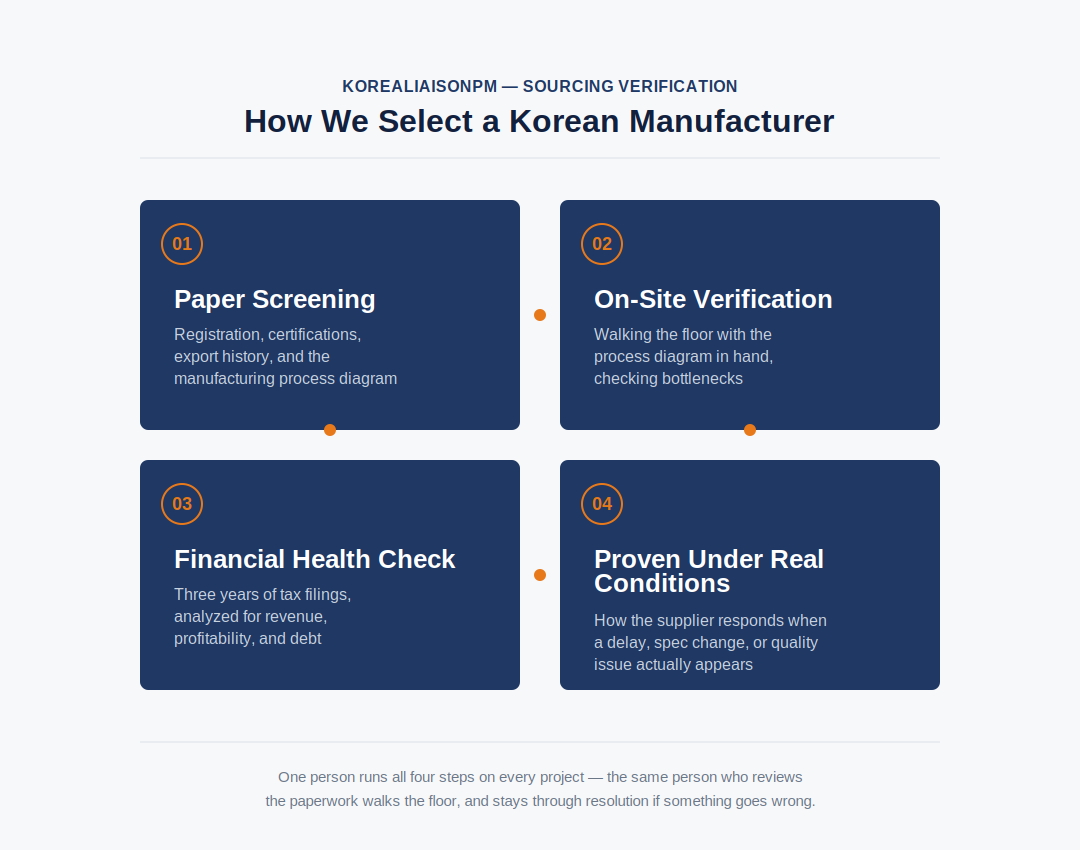
    Step 1: Paper Screening

    Before I visit anywhere, I start with documentation — business registration, relevant certifications (ISO and industry-specific standards), export history, and equipment lists. Beyond that, there are two things I always request: a company profile and a manufacturing process diagram.

    A company profile tells you how a company describes itself. A process diagram tells you something far more useful — the actual sequence of raw material intake, processing, inspection, packaging, and shipment, along with exactly where quality checkpoints sit within that sequence. A company with no process diagram, or one that’s suspiciously oversimplified, is itself a signal — it may mean the process was never standardized, or that things get handled ad hoc, project by project.

    This step looks simple, but it’s where most candidates actually get filtered out. A certification issued years before the equipment it supposedly covers was installed isn’t necessarily disqualifying on its own — but it raises a question: is this equipment still meeting that certification standard today? Any candidate that leaves that kind of question unanswered doesn’t move to the next step.

    Step 2: On-Site Verification

    This is where paper stops being enough. [Link: 10 Red Flags I Look For] The first thing I do on-site is walk the floor with the process diagram from Step 1 in hand, following it exactly. Does the actual line layout match the documented sequence? Are inspections actually happening at the checkpoints shown on the diagram? Are there any workaround steps in practice that don’t appear on paper at all?

    This is almost always where bottlenecks surface — work-in-progress piling up at a particular station, long wait times in front of certain equipment. What matters isn’t that a bottleneck exists; every factory has one somewhere. What matters is how the company handles it. Did they add capacity? Adjust shift scheduling? Or just let deadlines slip and hope no one notices? I ask directly, and I pay attention to whether the answer is specific or vague. A company that gives concrete numbers and concrete actions has clearly dealt with this problem before. A vague “we adjust as needed” is itself a warning sign.

    I also check whether equipment age matches what’s on paper, and look for small inconsistencies a certificate would never reveal — a tolerance range that doesn’t match what the machine is actually producing, a maintenance log that was clearly filled in all at once, a worker on the floor who isn’t the person listed as responsible on paper. None of this shows up as a yes/no on a checklist. It only shows up when you walk the floor yourself, diagram in hand, and ask.

    Step 3: Financial Health Check

    A factory can look solid on the floor and still be financially unstable — and that risk never shows up in a walkthrough. [Link: Financial Due Diligence vs. Factory Audit] For this, I request the company’s tax reconciliation statements, typically covering the past three fiscal years, and analyze revenue trends, profitability, and debt structure. From that, I put together a short internal assessment of whether this is a company likely to remain stable — and reliable — two or three years into a partnership. This matters because when a supplier runs into financial trouble, quality control and delivery reliability are usually the first things to break down. Less money means fewer people, and fewer people means quality suffers next. That sequence rarely changes. Most buyers never think to ask for this — but it’s often the difference between a supplier who delivers once and one who delivers for years.

    Step 4: Proving It Under Real Conditions

    Verification doesn’t stop once a supplier is selected. [Link: Case Study: Kazakhstan Copper Mine] [Link: Case Study: Aktogay] The real test comes when something goes wrong — a delayed shipment, a quality issue, a spec change mid-production. [Link: What Happens After Equipment Is Finished] That’s when a supplier’s real character shows, in ways no document or site visit ever could. Do they flag the problem early, or does it surface only after you catch it? Do they show up with a solution, or with an excuse?

    Comparing Candidates Side by Side — and the Problem with Scores

    Most buyers don’t decide based on a single candidate. They evaluate two, three, sometimes more, and choose one. A common approach here is checklist-based scoring — assigning points across categories and picking whoever adds up highest. Many audit firms use this method for good reason: when multiple auditors are evaluating multiple companies, standardized scoring keeps judgment from varying wildly from person to person.

    The problem is that a score measures whether something was checked, not whether it’s still true. A point awarded for holding an ISO certification counts the same whether that certification is five years old or was issued yesterday — even if the equipment behind it has completely changed since. A company without the certification, but with genuinely tighter process control, can end up scoring lower. Checklists guarantee consistency. They don’t guarantee that the consistent score reflects the actual risk.

    So when there are multiple candidates, instead of assigning scores, I lay out the actual findings from the steps above — especially on-site verification and financial health — side by side. Not “Company A: 92, Company B: 87,” but specific, concrete statements: this company’s floor matches its process diagram but handles bottlenecks poorly; that company has strong equipment but a debt ratio that’s been climbing for two years. What matters isn’t which number is higher — it’s which company is strong or weak, and exactly why.

    Why the Big Names Get Noticed First

    There’s another problem worth naming directly. Whether a company can communicate in English, holds international certifications, or has a dedicated export sales team — these are heavily weighted in most evaluation frameworks. None of them have anything to do with technical capability or financial health. And nearly all of them favor larger companies by default.

    The result is that genuinely strong small and mid-sized manufacturers — companies with excellent technical capability and solid financials — often never make it onto a shortlist at all, simply because they lack English-speaking staff or experience dealing directly with overseas buyers. Buyers never even learn these companies exist. Overseas buyers end up returning to the same well-known larger companies again and again, regardless of actual merit, while capable smaller manufacturers never get a fair shot.

    This is part of what I do on the ground. I speak the language, understand international business practices, and can package information the way buyers expect — which means I can close that gap on a company’s behalf. A strong manufacturer that had no way of reaching overseas buyers on its own gets evaluated on merit. And buyers, in turn, aren’t limited to the handful of names everyone already knows — they get access to real capability across a wider field.

    Why This Matters

    None of these steps are complicated on their own. What’s hard is doing them for every project, without exception, to the same standard. There’s always a temptation to skip the site visit when the schedule is tight, or skip the financial check when the paperwork looks clean.

    At larger sourcing firms, these steps are usually split across departments — sales handles documentation, quality handles the site visit, a separate due diligence team handles finances, and a PM handles it if something goes wrong. There’s a real advantage to this structure: expertise builds up at each stage, and it scales well for large projects. But when responsibility passes through that many hands, there’s always a moment where something can fall through the cracks of “whose job was that.”

    I run all of these steps myself, on every project. The person who reviewed the documentation and process diagram is the same person who walks the floor. The person who looked at the financials is still there if something goes wrong later. It’s not a structure built for running many large projects at once — but it’s built to make sure nothing on a single project gets missed.

    If you’re evaluating a Korean supplier and could use a second set of eyes on any part of this process, feel free to reach out.

    Want to check a candidate yourself first? Try our free Supplier Verification Checklist — it walks through the same four steps above and takes about two minutes.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • Case Study: The Second Kazakhstan Project — A Client Who Came Back Without Being Asked

    Case Study: The Second Kazakhstan Project — A Client Who Came Back Without Being Asked

    Not every project has a dramatic crisis. But no crisis doesn’t mean there’s no story.

    The Bozshakol project — the truck wash system I built for a copper mine in Kazakhstan — was chaotic from start to finish. Drawings arrived late, the timeline was tight, and I was solving problems on the spot at every stage. If you’ve read that story, you know how it ended: the audit passed, the system worked, and the client was satisfied.

    There’s a part of the story I haven’t told yet. It happened about eight months later.

    A Direct Request, No Introduction Needed

    The first project came to me through an Australian partner company who had served as the client’s point of contact at the time. Somewhere along the way, that partner became unreachable. KazMinerals tracked down my own contact details — I had led the first project — and emailed me directly, asking whether I could install a similar washing system at their Aktogay site.

    It wasn’t a referral, and it wasn’t a new RFQ sent out to a shortlist of vendors. A client who had already tested the relationship once came back on their own. I told them I’d review the project and get back to them.

    The Site Had to Be Checked Again

    The equipment itself was similar to Bozshakol, but the site was different. This wasn’t something I could confirm from paperwork alone — the drawings and the actual installation location needed to be checked in person, so I traveled to Kazakhstan with our design engineer.

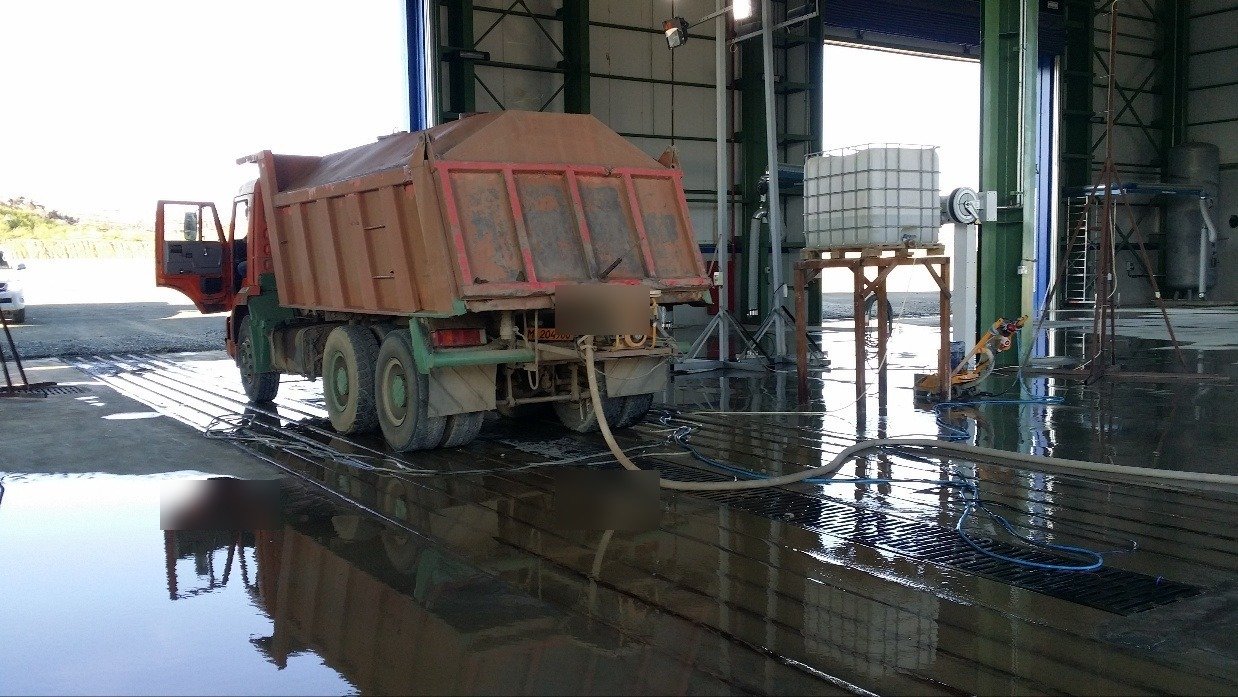
    Drainage trench under construction at the Aktogay washing facility site

    I stayed on site to coordinate the overall schedule while our design engineer and a KazMinerals engineer went out to the installation site to compare the drawings against the actual conditions, point by point. A different terrain can mean a pipe route or an installation height that no longer matches the drawing — this was not a step we could skip.

    While waiting for their findings, I got a call from our design lead: the drawings, fortunately, only needed minor adjustments. Given how small the changes were, I told the local purchasing contact we’d handle the drawing revisions at no extra charge. The equipment and piping, though, needed some changes, so I asked for their understanding — I’d need to go back to Korea and requote with our subcontractors.

    Back in Korea, Requoting the Project

    Back in Korea, I met with our subcontractors one by one to work through the numbers. I didn’t add a design fee, but documentation and testing costs had to be reflected. Once those were built into the final quote, we negotiated the terms and the project was confirmed.

    This Time, the Challenge Was Time

    The client had one main request: pull the schedule in, noticeably shorter than the first project. Having done this once before made it possible to agree to it. Actually hitting that schedule was a different matter entirely.

    With less room for error, a single subcontractor slipping on their timeline could have thrown off the whole schedule. So I ended up checking in with our subcontractors more often than I had on the first project — tracking material deliveries and machining schedules day by day to make sure nothing slipped. There was no single dramatic event this time. Instead, there was a lot more attention paid to the details, every single day.

    When we made it through packaging and shipment without a single delay, it was genuinely satisfying. And not long after, I got an email from the client thanking me for pulling the schedule in and delivering without issues — a message I still remember well.

    Why This Is the Story

    It’s tempting to think a case study needs a crisis to be worth reading. But for a buyer evaluating a sourcing partner, a story like this one can be more convincing than a rescue story. The client came back without hesitation because the first project had been done right — and this time, I had to prove the same result was possible under harder conditions: a much tighter schedule.

    This is what a sourcing relationship should look like once the hard part is over. Not a dramatic rescue, but the ability to deliver the same result under slightly harder conditions, again and again. Aktogay was a test of whether that trust was real — and it was.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • The Second Chance — How One Project Led to Another, Across Europe

    The Second Chance — How One Project Led to Another, Across Europe

    Part of an ongoing series on how Korean sourcing and manufacturing projects actually run. The last post covered a quality crisis on my first engine program with a major automotive alliance and the three weeks I spent resolving it overseas. Handling that crisis quickly and fairly turned out to open the door to a second project almost immediately.

    A second bid, built on trust

    Once we’d resolved the earlier quality issue in a way the customer could genuinely accept, a second bidding opportunity came our way. We submitted a quote through the normal process, went through technical meetings at the automaker’s overseas headquarters, and after a final round of price negotiation, won the business over several competing suppliers.

    This engine was different from the first — a compact diesel platform used not just by this alliance but across several automakers’ small-car lineups. Volume started in the hundreds of thousands of units annually, with real potential to climb into the millions as adoption spread to additional brands. For our company, this was a major program, and headquarters had high expectations for it too. Unlike the first project, this engine wasn’t assembled at the same plant as before — it was built at a different plant, further south in Europe, which meant our prototype deliveries shifted there as well.

    During early prototype development, I was overseas often, and the customer’s team visited our factory just as frequently — checking that our actual production process matched what we’d submitted on paper, and given our recent history with a quality escape, auditing our containment procedures in far more detail than before.

    Video calls every other day, for months

    Normally, you’d coordinate logistics with a purchasing contact at headquarters and handle technical questions separately with the engineering team. This project ran differently. The customer assigned a dedicated PM, and that person and I handled nearly everything together, from development kickoff onward — an unusual setup.

    We worked from a shared requirements sheet and held video calls with each other roughly every other day. I’d send over whatever documentation we owed by email, we’d update the sheet together, and cross off anything that wasn’t realistic or necessary for us to produce. From the start of development through prototype delivery and engine testing, this went on for months — two or three video calls a week, with in-person visits to headquarters whenever needed. I kept our internal teams updated on progress throughout.

    Somewhere in the middle of those months, I started half-joking with the PM that once development wrapped and I made it to headquarters, they owed me pizza and beer.

    An unexpected dinner invitation

    Once development testing wrapped up cleanly and I traveled to headquarters for final wrap-up work, something I hadn’t expected happened. A senior executive personally invited me to dinner, thanking me for the work — it turned out my running joke with the PM had made its way up the chain.

    As it happened, our company’s CEO’s son (a director at the time) was also visiting headquarters that day for an unrelated event, but the dinner invitation had only been extended to me. When I mentioned the situation, the executive asked whether he could join too, and after checking with the PM, got the go-ahead. We were treated to a genuinely excellent dinner at a fine restaurant, and at the table, the executive told me directly that the development process couldn’t have been easy, and thanked me for seeing it through.

    Hearing that in the moment meant more than I expected — being recognized like that is rare in a supplier-customer relationship. It’s the kind of acknowledgment that can be hard to get even internally, no matter how much you deliver, so hearing it from the customer instead made the whole stretch feel worth it.

    Prototypes, and a trip back overseas

    Once prototypes shipped to the new plant, the PM asked me to come see the engine assembly in person. The same executive from headquarters said he’d be there too. Our CEO asked that his son (a managing director by then) come along as well, so the two of us flew in, took a train to the plant, stayed overnight, and toured the assembly and testing process the next day. That evening we had dinner with the PM, the executive, and the CEO’s son, talked through a range of things, and flew home with what we needed to wrap things up.

    A minor defect, and a solo trip back

    Some time later, once things were running smoothly, a defect turned up in a batch of around 1,000 units — nothing close to the severity of the earlier crisis, thankfully. This time I went alone. I met with the plant’s quality manager, reviewed the flagged units, and with their help brought in two sorting staff to work through them together. (Plants like this typically keep a pre-arranged sorting contractor on standby for exactly this kind of situation.)

    Sorting turned up around 450 confirmed defective units; the rest were cleared for use. I asked our team to ship the remaining volume by sea rather than air, since this situation wasn’t urgent enough to justify the added cost. I wrapped things up and flew home.

    What both projects taught me

    Both projects, in their own way, also made clear the limits of working at a small or mid-sized supplier — one person ending up responsible for technical sales, development, quality response, and even production line planning, all at once. But within those limits, the approach stayed the same: face the problem directly, and build the relationship on trust rather than excuses. That’s the principle that’s carried through the rest of my career since.


    This is part of an ongoing series on Korean manufacturing and sourcing project management.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • Becoming a Global Automaker Supplier — The Alliance Audit, and Three Weeks Overseas I’ll Never Forget

    Becoming a Global Automaker Supplier — The Alliance Audit, and Three Weeks Overseas I’ll Never Forget

    Part of an ongoing series on how Korean sourcing and manufacturing projects actually run. Earlier posts covered recent projects — this one goes further back, to my time at a Korean auto parts manufacturer, where I first went through the process of becoming a supplier to a major European automotive alliance.

    The first gate — the alliance’s supplier evaluation standard

    Any parts supplier looking to work with a major automaker eventually runs into a process like this: a joint quality standard the alliance uses to evaluate a supplier’s quality management system and production processes. It scores several areas — quality management, defect analysis, quality target-setting, project management, process FMEA, shop floor processes, and more — on a numeric scale, and rolls that up into a final grade.

    Here’s the part people often don’t expect: passing an audit with the local subsidiary in Korea doesn’t automatically qualify you to bid on business with the automaker’s overseas headquarters. To supply the parent company directly, headquarters sends its own audit team to evaluate you separately, and you need a minimum grade before you’re even eligible to bid. Only after clearing that grade do you get access to the supplier portal to see open tenders.

    Preparing for the audit was its own project. All the evaluation criteria documents came from headquarters in English, and at the time there was almost no reference material translated into Korean. So I translated all of it myself and distributed it department by department, so each team understood exactly what the customer expected and could prepare accordingly. Once that groundwork was done, every document needed for the actual audit day had to be re-prepared in English and sent to the audit team in advance, so they could bring it with them when they visited the Korean factory and verify that what was on paper matched what was actually happening on the floor.

    I still remember the tension of audit day itself. I gave the presentation myself, in a room that included senior purchasing executives from headquarters, directors from the local subsidiary, and our own company’s leadership. I was still fairly green at the time, and the systems involved were a lot to fully grasp — but I opened with a greeting in halting local language, which got a surprisingly warm reaction, and the presentation went smoothly from there. The hardest part came after: over an hour of walking the factory floor under close scrutiny. We came out of it with a strong grade, which is what earned us the right to bid at all.

    Growing into technical sales

    I had been working in investment-related roles in Seoul when an acquaintance recommended me for a position at a Korean auto parts manufacturer. I started on the overseas business side, and quickly realized that handling RFQs properly meant understanding production, machining, quality, and quality management from the inside — so I rotated through each department before eventually landing in the technical research division, where I began working in technical sales in earnest.

    Around that time, we won development work for a European automaker’s bracket component, but the automaker ran into financial trouble not long after, and the project never made it past the development stage into production. The company then pivoted toward other major global automakers, winning business with one U.S. manufacturer while also clearing the alliance audit described above.

    From there I worked technical sales roles connected to well-known German and American automotive suppliers and manufacturers, traveling across Europe. Even after I was later recruited to a different company, the relationships I built during this period stayed with me.

    An engine component order, and a phone call before dawn

    After clearing the alliance audit, we won an order for a component going into a mid-size diesel engine platform. That engine was assembled and tested at a plant in Europe before going into the alliance’s premium SUV lineup, and our parts shipped on the same production schedule.

    Passing an audit rarely means you’re handed a large order right away. You first have to prove yourself on a small development run before you’re even considered for full production volume. We cleared the development stage cleanly — prototype delivery and engine testing both passed without issue — and the company moved into mass production, shipping steadily to that assembly plant.

    About seven or eight months into mass production, my phone rang before dawn. It was the overseas purchasing contact, sounding urgent. When I asked what was wrong, he said the assembly plant was running leak tests after engine assembly, and water was getting through. They didn’t know exactly where it was coming from, but they suspected it was our part.

    I called our technical director immediately to brief him and have him report to our CEO. I also asked the overseas purchasing contact to have the plant’s engine test manager photograph the affected area in detail and send it to me by email. When I checked my inbox after getting to the office, it was confirmed — the leak was coming from our part. At the joint where we supplied the fitting, high pressure was gradually working the pipe connection loose. I remember feeling like the floor had dropped out from under me.

    The cause, and three weeks that started overseas

    The root cause turned out to be a subcontractor who had changed a component specification without authorization. Design changes like that are never supposed to happen without notifying the customer and getting sign-off. Everything had been fine before the change; the problem started only after the revised spec went into production. Worse, thousands of parts built to the flawed spec had already shipped.

    Late that afternoon we held a video call with the overseas purchasing team, the assembly plant’s director, and the assembly manager — the mood was as serious as it gets. After instructing each department to prepare a root-cause analysis and countermeasure plan (an 8D report), I flew out immediately along with our machining manager and our technical research director.

    Watching the leak test in person and inspecting the affected engines, the situation turned out to be worse than we’d feared. Some engines had already been transferred to another brand under the same alliance, destined for actual vehicle assembly. The customer’s team argued that even previously-passed units couldn’t be trusted anymore, that this was a recall situation, that we should bear every cost, and that we should also compensate them for the line stoppage.

    How do you respond to that? I held my ground. I told them that if we accepted those terms, our company wouldn’t survive — that the fault was clearly ours and we’d take full responsibility for fixing it, but escalating the situation beyond what was necessary wasn’t fair to anyone. Then I walked the room through the data we’d brought from Korea, point by point. I asked for time to check lot numbers — both the parts still in inventory and the ones already installed in engines — and once we had that, proposed that engines built with the affected lot be disassembled and reworked at our cost, while engines built with unaffected lots could be re-tested for leaks and shipped on to the next assembly plant as planned. When they asked whether I could actually stand behind that, I told them I would — after getting confirmation from our technical director, our machining lead, and ultimately our CEO.

    That’s when three weeks of what felt like trench warfare with the local plant began. There was no way to inspect thousands of parts individually in the time we had, so we had to sort by the lot markings on each pallet. Our technical director and machining manager flew home the next day, leaving me there alone to run the sorting process at the plant every day. The plant manager told me I’d need to move to a hotel closer to the site since I’d be coming in daily — so I did, showing up before dawn each morning to work through the parts with two sorting staff the plant assigned. Every evening I’d get an update from Korea, bring the new data into the plant the next morning, hear “this isn’t convincing enough, the countermeasure isn’t sufficient,” and request another round of data from Korea. It repeated like that, day after day. I didn’t have time to see any of the local sights — it was just the hotel and the plant, back and forth.

    Once the replacement parts had finished production in Korea, the company decided to air-freight them out to avoid the line-stoppage penalty ballooning further — air freight alone cost over ten million won. I asked the overseas purchasing contact to arrange expedited customs clearance in advance, and the moment we landed, staff were already pushing carts through the process. We loaded the parts onto a truck and drove several hours before dawn from the airport to the plant, opened the back gate, and handed the parts straight to the assembly line. Only after I’d sent photos and confirmed everything by phone with the purchasing contact did I finally get a moment to breathe — standing on an empty street before sunrise with a cigarette, feeling something close to relief for the first time in weeks. It really was that intense.

    Even after that, there was a long back-and-forth over the claim costs. Our headquarters wasn’t willing to concede everything the customer wanted, and the customer kept pushing for more. After a genuinely difficult stretch of negotiation, both sides eventually landed on terms they could accept. Three weeks after I’d arrived, I finally slept through an entire night for the first time. I said my goodbyes to the plant staff I’d come to know over those weeks, had dinner with the purchasing contact, and flew home.

    What this experience taught me

    The biggest lesson from that whole ordeal was this: build a timing schedule with a remarks column, and check progress against it every single week. The weekly-tracking approach I now bring to KoreaLiaisonPM projects genuinely traces back to this experience. The next post covers a follow-on engine component project with the same alliance, at a different plant further south in Europe.


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →
  • Case Study: Building a Truck Wash System for a Kazakhstan Copper Mine — From Drawing Chaos to a Successful Audit

    Case Study: Building a Truck Wash System for a Kazakhstan Copper Mine — From Drawing Chaos to a Successful Audit

    Part of an ongoing series on how Korean sourcing and manufacturing projects actually run, told through real projects rather than general advice.

    Why mines need wash systems at all

    If you’ve never worked in mining, this might sound like an odd thing to build a business around. Here’s the short version.

    Most open-pit mines in places like Australia, China, and Kazakhstan run enormous haul trucks — machines that can cost well over a million dollars each. Once these trucks start hauling ore, the undercarriage and chassis are exposed to constant abrasive buildup, and components corrode and wear out far faster than they should. A proper wash system — high-pressure underchassis spinners, wash arches for the upper body, a drying stage, and a full water reclamation and filtration loop — extends the life of that equipment dramatically. Compared to replacing a haul truck, the cost of a wash system is easy to justify once a mine operator actually sees the math. That’s the market this project sat in.

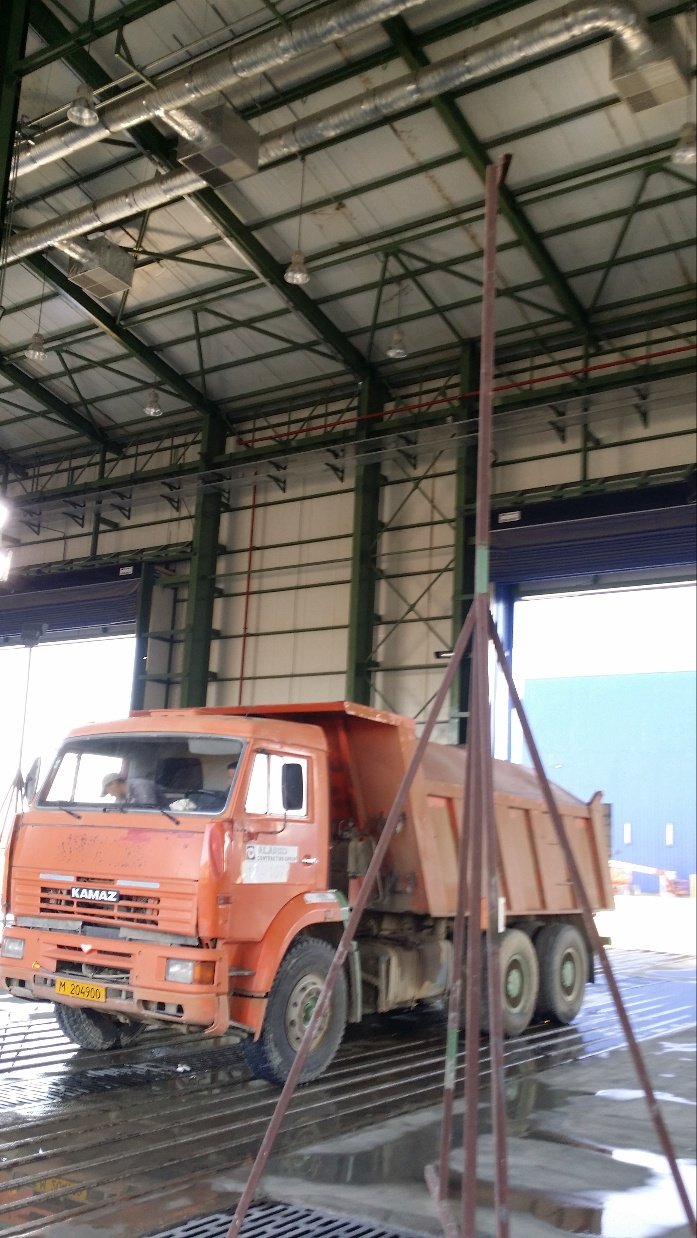
    On site at Bozshakol, Kazakhstan, during the design verification visit.

    The client chain looked like this: Kazakhmys (the mine operator in Kazakhstan) engaged AMMS Group, an Australian engineering company, for the wash system design and supply. AMMS in turn brought the project to JAM, a Korean–Australian joint venture, to handle the full scope — design, manufacturing, and delivery of the entire wash system. I managed the project on JAM’s side.

    The scope covered the full system: three large custom pumps (developed with Wilo specifically for this application, since nothing off-the-shelf fit), motors, general drainage pumps, the complete piping run for the wash bay, main and auxiliary electrical panels (shipped pre-installed inside a container), multiple wash-water cannons, mounting plates for all equipment, and the full water treatment and filtration system including sludge filtration.

    Design alone took about two months. From kickoff to a confirmed, signed-off design from Kazakhmys took roughly four months total. Manufacturing and production took around nine months, including shipping. Once the finished equipment left port, ocean transit plus customs clearance in Kazakhstan and inland trucking to the mine added another 40–50 days.

    The drawing problem nobody expected

    A roadside stop along the way to the mine — a reminder of just how remote these sites can be.

    Before finalizing our own design, we visited the actual site — Bozshakol mine — to verify the space where the wash system would be installed. This turned out to be the right call, because the reference drawings that had been passed down the chain (Kazakhmys → AMMS → JAM) didn’t match the real site at all.

    What happened was that AMMS had been paid by Kazakhmys to produce site drawings, but those drawings were unusable. So on top of our own contracted scope — the full wash system design, piping, and electrical panel layout — we ended up redrawing AMMS’s site foundation drawings from scratch, with no additional payment, simply because the project needed it to move forward and we’d already committed to delivering.

    If we hadn’t insisted on the site visit early on, we would have designed the entire system around drawings that didn’t reflect reality. The equipment likely wouldn’t have fit on installation, the claims and rework costs would have been significant, and it would have damaged the trust we’d built with everyone in the chain. Catching this early, before a single part was fabricated, is the kind of thing that never shows up in a contract but ends up mattering more than almost anything else.

    Running the schedule

    Once Kazakhmys gave final written confirmation on the design, I notified all the subcontractors that they could begin — with a commitment that material costs would be wired to them within the week, so they could move without waiting on paperwork. Internally, JAM built a timing schedule and distributed it to every vendor involved.

    From there, it’s the same weekly-visit, remarks-column discipline I’ve described in earlier posts: track progress by vendor, log any issues in a remarks field, and only escalate the ones that actually affect the client’s delivery date rather than reporting every minor hiccup. I also try to physically visit factories once or twice a week when possible, even though vendors are often spread across different regions. It’s not always easy, but it matters — specs that look identical on paper (Korean standards vs. Australian vs. Kazakhstani, even under a shared reference like ASTM) get interpreted slightly differently by welders and fabricators who default to whatever they’re used to. Regular site visits are really the only way to catch that drift before it becomes a real problem.

    Three days before the audit

    Everything else on this project went smoothly. Then, three days before Kazakhmys’s own inspection firm was scheduled to audit the completed system, a problem surfaced in the piping and electrical work — from a vendor that had shown no warning signs at all up to that point.

    We split into two teams — one on the piping issue, one on electrical, including myself — and worked through it around the clock for three days. Nobody went home. We kept both the client and the inspection firm informed throughout, and asked for a short grace window in case we needed it. In the end, both issues were resolved in time, and the system passed audit on schedule with no delay to the delivery date.

    Because the electrical panel is the system’s core — if it fails, nothing runs — I wasn’t comfortable simply handing it off after the fix. Normally, sending an engineer on-site for installation support is a paid service the client requests separately. For this project, I chose to cover that cost myself and sent one of our engineers along with the panel vendor’s engineer to be present for the actual installation, train the local team, and run the first startup themselves. Both engineers told me afterward it was one of the more rewarding parts of the project.

    The client’s reaction to all of this was, understandably, very positive. We’d already fixed a serious problem three days before their own audit without missing the deadline, and then covered the cost of sending an engineer on-site ourselves rather than billing for it. That combination did more for the relationship than anything I could have said in a meeting.

    Eight months later, Kazakhmys came back to us directly for a second wash system project — this time at their Aktogay mine, and this time with no AMMS Group in between. That, more than anything else, is what tells me the first project worked the way it was supposed to.

    Getting paid, and getting it shipped

    Once the audit was behind us, there was still the commercial side to manage. This was the first time JAM and Kazakhmys had worked together directly for payment — funds flowed straight from Kazakhmys to JAM, bypassing AMMS in the payment chain — so there was naturally some caution on both sides. The interim payment came through about a week to ten days after the audit, once we’d shared photo documentation of the equipment in storage and confirmed the final stages of production. Vendors are waiting on that money too, so managing both sides of that gap is honestly one of the less glamorous parts of being a PM.

    With the interim payment in, we moved into final assembly and packaging — all built to the design drawings, with the piping shipped disassembled for site assembly. Packaging planning starts about a month before shipment, coordinated with both the packing contractor and the freight forwarder so containers are booked to match the actual crate dimensions; large equipment leaves very little room for error here. On packing day, every container was photographed as it was loaded, sealed, and photographed again after sealing. Those photos went to the client along with the shipping documents, and once they confirmed everything, the final balance was paid and the containers shipped.

    After that, the last piece was putting together the technical documentation package — approved final drawings, assembly instructions per piece of equipment, operating manuals, and a troubleshooting guide — bound into physical manuals and mailed to the client. As mentioned above, we also sent an engineer for on-site installation support on this one.

    What I’d want a buyer to take from this

    None of this went perfectly. The drawings were wrong, a vendor had a last-minute problem nobody saw coming, and the payment structure was new territory for everyone involved. What actually got the project through wasn’t avoiding those problems — it was catching the drawing issue before fabrication started, keeping the client informed rather than hiding the panel issue, and being willing to eat a cost (redrawing AMMS’s site drawings, sending an engineer without extra billing) when it protected the outcome. That’s really the whole approach — and Aktogay, eight months later, was the proof it worked.


    This is part of an ongoing series on Korean manufacturing and sourcing project management. Previous posts cover timing schedule management, handling production problems, packaging and shipping, technical documentation, and engineer dispatch as general processes — this one walks through how they actually played out on a real project. For an earlier chapter in this story — how I first became a supplier to a major automotive alliance and navigated a major quality crisis overseas — see “Becoming a Global Automaker Supplier.”


    Written by Cheolho Shim, founder of KoreaLiaisonPM in Busan. Twenty years in automotive OEM supply chains and mining infrastructure projects. About me →